50 Years Of Trust | Engineering The Next Energy ERA
50 Years Of Trust | Engineering The Next Energy ERA
At ISOTEX, sustainability is not a policy — it is the engineering philosophy behind every boiler and thermic fluid heater we build. From biomass-fueled systems to CPCB-compliant emission controls, every ISOTEX solution delivers thermal energy with minimal environmental impact.
Waste-to-Energy FBC | SMARTWIZ IoT | 1–50 TPH Steam | 2L–1.5Cr Kcal/hr | 75+ Countries | 10,000+ Installations | Est. 1978
For nearly 50 years, ISOTEX has delivered thermal energy solutions trusted by industries across India and the world. Our commitment to sustainability shapes every design decision — from raw material sourcing to after-sales service.
“
The most sustainable boiler is not just one that burns cleaner — it is one that wastes nothing. Every unit of fuel saved is a unit of emission avoided. That has been our engineering principle since 1978.
— ISOTEX Engineering Philosophy | www.isotexglobal.com
ISOTEX pioneered multi-fuel and biomass boiler technology in India, enabling industries to move away from fossil fuels using agricultural waste, wood chips, pellets, and industrial residues.
Every ISOTEX project is backed by documented energy consumption data. Our customers report average fuel savings of 10–25% after switching to ISOTEX optimised systems.
From pharmaceutical plants in India to textile mills in Southeast Asia, ISOTEX solutions help industrial buyers meet their corporate ESG targets and government emission norms.
ISOTEX’s sustainability strategy is built on four interdependent pillars — covering fuel choices, emission management, energy intelligence, and manufacturing responsibility.
ISOTEX boilers and thermic fluid heaters are designed to run on biomass, agro-waste, pellets, wood chips, and multi-fuel combinations — reducing dependence on coal and fossil-based fuels. Customers in the Plywood, Textile, Paper, Edible Oil and Chemical industries regularly run on near-zero-cost agricultural residues sourced locally.
Biomass | Pellets | Agro Waste | Multi-Fuel | Co-Firing | Wood Chips | Rice Husk | Bagasse
All ISOTEX systems meet CPCB emission norms. Our integrated pollution control options — multi-cyclone, bag filters, wet scrubbers, and Electrostatic Precipitators (ESP) — ensure clean stack emissions across all fuel types and capacities, from 1 TPH to 50 TPH.
CPCB Compliant | Bag Filter | ESP | Wet Scrubber | Multi-Cyclone | SPM Controlled
The SMARTWIZ IoT platform provides real-time boiler monitoring, predictive fault alerts, and automated fuel optimisation — reducing waste by up to 15% from Day 1 of installation. Retrofit-compatible with any existing ISOTEX boiler or thermic fluid heater, without production downtime.
SMARTWIZ IoT | Real-Time Monitoring | Predictive AMC | Remote Diagnostics | Fuel Optimisation
Every product in this range is designed specifically to reduce fossil fuel dependency, lower emissions, and maximise thermal efficiency for Indian and global industries.

ISOTEX’s flagship green product. Accepts 15+ types of solid biomass fuels including rice husk, bagasse, wood chips, sawdust, mustard stalks, and more. IBR-certified, available from 1 TPH to 30 TPH with optional multi-fuel configuration. Near-zero carbon emissions when running on agricultural residue.
Capacity: 1–30 TPH | Efficiency: 82%+ | Fuel Types: 15+ | Certification: IBR

83% thermal efficiency with the cleanest solid-fuel combustion profile. Uniform pellets ensure consistent heat output — ideal for Pharmaceutical, Food, and Textile industries requiring precise temperature control and CPCB-compliant stack emissions.
Range: 2L–30L Kcal/hr | Efficiency: 83% | Fuel: Wood / Biomass Pellets
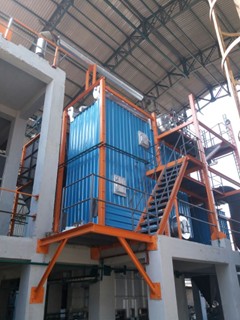
Burns low-grade waste fuels — high-ash coal, agro-residue, textile dust, industrial waste — with superior combustion efficiency. A true circular economy solution for large-scale heat generation. Capacities from 5 TPH to 50 TPH.
Range: 5–50 TPH | Fuel: Mixed Waste / Agro Residue
Switch between solid biomass and oil/gas fuel as per market price fluctuations. Built-in fuel optimisation ensures lowest operating cost without compromising steam quality or pressure stability. IBR certified across all configurations.
Retrofit any existing ISOTEX boiler with real-time monitoring, remote diagnostics, and automated combustion control. Reduce fuel waste by 10–15% immediately after installation. Compatible with all Ecobloc CS and Ecotherm TFH models.

Recover up to 80% of condensate from steam systems — reducing water consumption, chemical costs, and boiler blowdown losses. Essential component of any sustainable, low-operating-cost boiler house.
With nearly five decades of experience across India’s most energy-intensive industries, ISOTEX is uniquely equipped to lead the energy transition — not as a bystander, but as the engineering partner driving it.
“Indian industry is at an inflection point. ISOTEX has anticipated this shift for years — and our product roadmap, technology investments, and manufacturing capabilities are already aligned to this new reality.”
Regulatory pressure, rising fossil fuel costs, ESG mandates from global supply chains, and voluntary sustainability commitments are compelling manufacturers to rethink how they generate and consume thermal energy.
ISOTEX’s quality and compliance framework has been built over five decades to meet the most demanding global standards. Our certifications are the foundation of customer confidence across 75+ countries.
Our engineering team responds within 24 hours. Share your capacity requirements and fuel preference. We’ll engineer the right solution.
WhatsApp us